Introduction
In the ever-evolving world of cosmetic packaging, the significance of package compatibility testing for cosmetic packaging cannot be overstated. It’s a crucial aspect that ensures the seamless interaction between the packaging material and the cosmetics it contains. This article delves into the definition of compatibility testing, its various types, real-world cases in cosmetic packaging, and the essential practices for conducting comprehensive tests.
Definition of Compatibility Testing
Compatibility testing in cosmetic packaging involves evaluating the interaction between plastic packaging and cosmetics. It encompasses three main types: chemical compatibility, physical compatibility, and biological compatibility.
Chemical Incompatibility
Chemical incompatibility arises when the chemical components of the cosmetic packaging material react adversely with cosmetic ingredients, leading to issues such as material yellowing or changes in odor.
Biological Incompatibility
Biological incompatibility occurs when substances from the cosmetic packaging material migrate into the cosmetics, surpassing safety standards. Harmful substances like plastic additives, solvents, volatile organic compounds, and hazardous metals can pose risks.
Physical Incompatibility
Physical incompatibility involves changes in the cosmetic packaging material and its contents due to mutual influence. This can manifest as infiltration, adsorption, cracking, and dissolution.
Understanding Compatibility Test Results
Compatibility test results for cosmetic packaging are intricate, often raising questions about why certain samples exhibit issues while others do not under the same conditions. The reality is that compatibility failures exist at a certain rate, making assessing a broader sample size imperative to uncover potential problems in mass production.
Compatibility Accident Cases in Cosmetic Packaging
Case One: Sunscreen Ingredients and PET Containers
A luxury goods company faced issues when sunscreen ingredients proved physically incompatible with PET containers, leading to cracking. This incident prompted a shift to materials with more suitable properties for cosmetic packaging, emphasizing the importance of material selection.
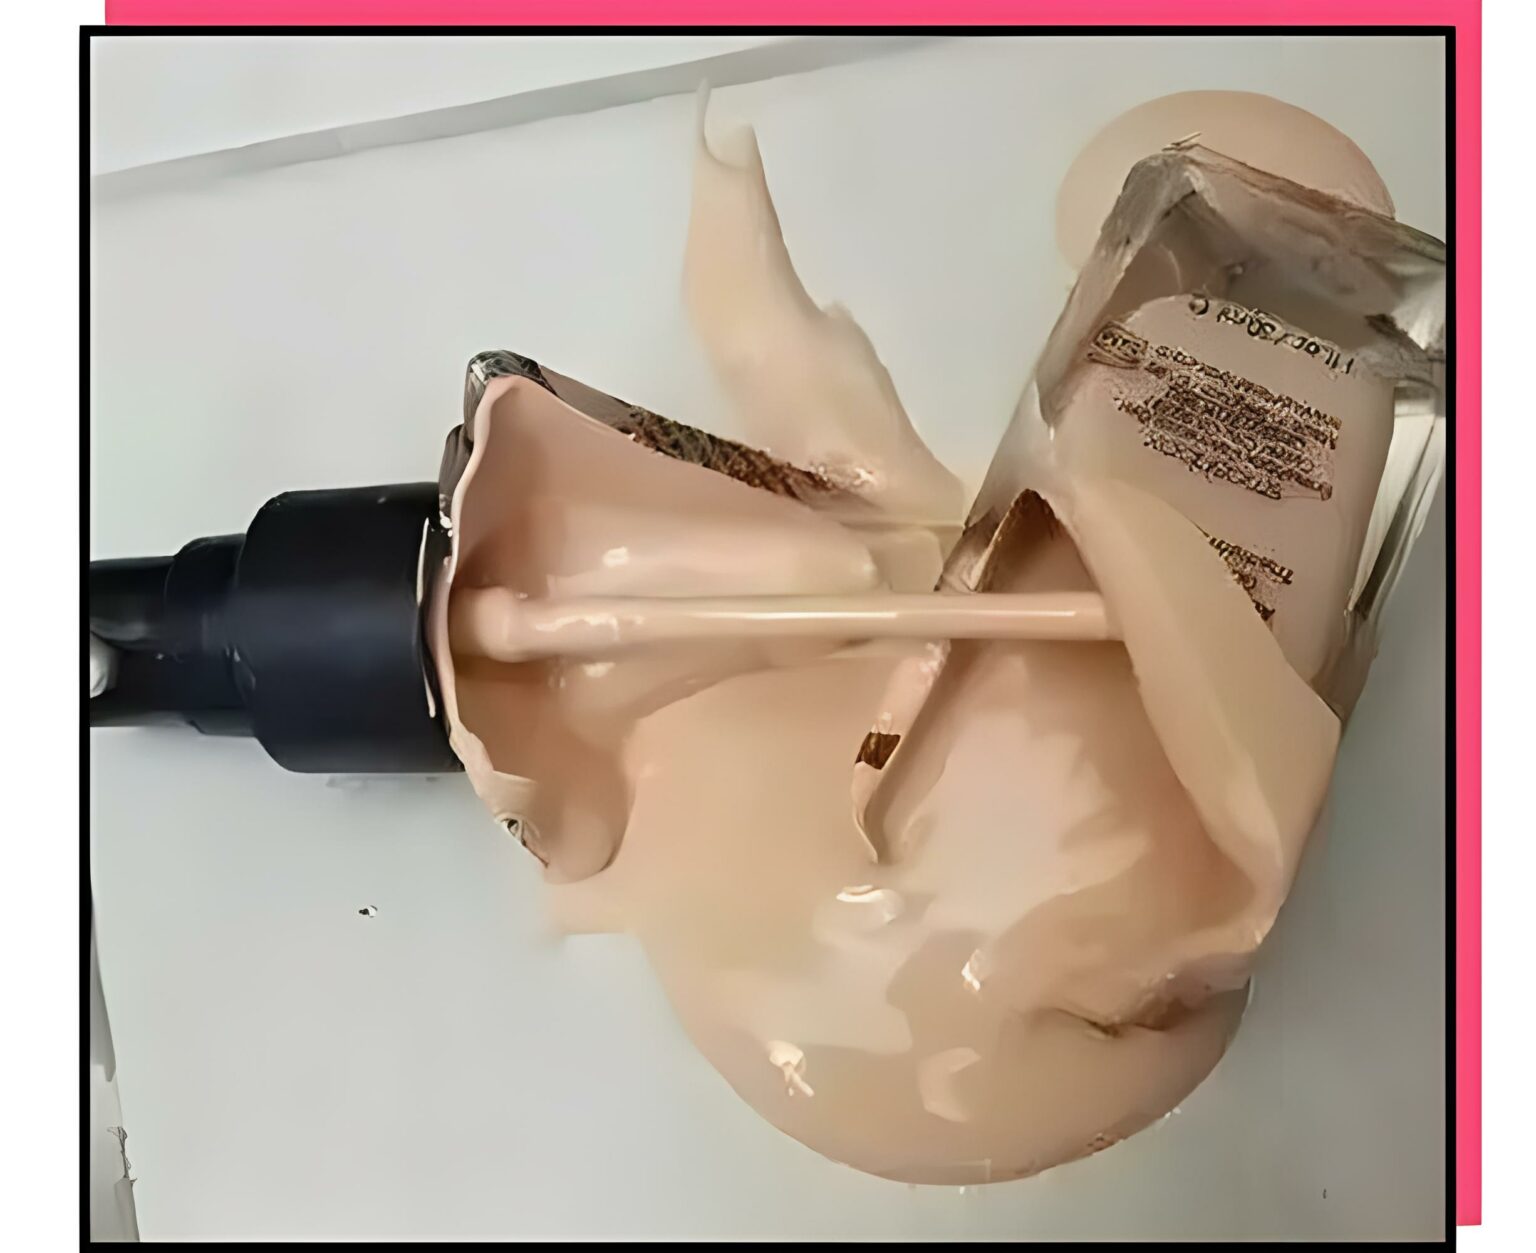
Case Two: Color Changes in Foundation Product
A cosmetics giant experienced color changes in a foundation product due to pigmentation from the cosmetic packaging material. This case highlights the necessity of compatibility testing even when changes seem minor.
Core Packaging Compatibility Tests — What to Run and Why
Weight Loss Test (Leakage and Evaporation)
The weight loss test determines whether a sealed, filled package loses product weight over a defined period under controlled or stress conditions. It is the most important test for alcohol-containing formulas, fragrance-heavy products, and any product that will be shipped by air or stored in warm environments.
Procedure (standard method): Fill the package to its recommended fill level with the actual formulation. Record the initial weight of the filled, sealed package to four decimal places. Store at 40°C / 75% RH for 4 to 12 weeks (the duration and conditions should match the target market’s regulatory requirements or the brand’s internal specification). Reweigh at defined intervals. Calculate percentage weight loss per week.
Acceptable threshold: This varies by regulatory market and product type. EU cosmetic brands commonly target <0.5% weight loss over 8 weeks at 40°C as a pass criterion for alcohol-containing products. Confirm the applicable standard for your target market.
Common failure scenario: A 100ml aluminium-cap glass toner bottle passes weight loss at ambient temperature but fails at 40°C because the aluminium cap liner is not rated for the alcohol content of the formula. The solution is either a different cap liner specification or a switch to a ROPP aluminium closure with an inner liner rated for high-alcohol formulas.
Stress Crack Test
Stress cracking is an invisible failure mode — the packaging passes visual inspection at delivery, but develops micro-cracks during storage that eventually become full fractures or leakage points. It is most common in PETG under contact with certain formula components, and in PP under contact with some surfactant or solvent combinations.
Procedure: Fill the package to the recommended level with the actual formula. Store upright and inverted at elevated temperature (commonly 40°C–50°C) for 4 to 8 weeks. Inspect under magnification for crazing, stress marks, or visible cracks, particularly at the shoulder, base, and any geometric stress points on the package.
High-risk formula components: Surfactants (SLS, SLES, coco-glucoside), limonene and other terpenes, high-concentration essential oils, propylene glycol, some solubilising agents, and UV filters used in sunscreen formulas.
Common failure scenario: A PETG jar filled with a face cream containing a surfactant blend and limonene at 1% develops stress cracking at the shoulder after six weeks at 40°C. The solution is a switch to PP (more chemically resistant to this combination) or a reformulation of the fragrance component to reduce limonene concentration.
Pump Compatibility and Dispense Consistency Test
A pump dispenser is specified with a nominal output per stroke (for example, 0.5cc ± 15%) at a defined viscosity range. When the actual formula viscosity differs significantly from the pump’s design range, dispense output, consistency, and priming behaviour can all be affected.
Procedure: Fill the package to the recommended level with the actual formula. Test prime time (how many strokes before first dispense), output per stroke (weigh 10 consecutive strokes, calculate mean and standard deviation), and behaviour at the low-fill level (the last 15% of fill). Repeat at the temperature extremes the product will experience in distribution.
High-viscosity failure scenario: A pump specified for serums (viscosity 2,000–8,000 cP) is used with a rich facial cream (viscosity 25,000–80,000 cP). The pump requires 15–20 strokes to prime on first use, and dispense output varies by more than 30% per stroke. The solution is either a pump upgrade to a high-viscosity specification or a formulation adjustment.
Low-viscosity failure scenario: A pump specified for cream is used with a very thin toner (viscosity <200 cP). The dip tube inlet is too large for the thin formula, causing dripping and inconsistent output at an angle. The solution is a pump with a dip tube check valve rated for low-viscosity products.
Transit and Drop Test
Products sold through e-commerce or international distribution face physical and thermal stresses that are significantly more severe than retail shelf distribution. Transit testing simulates these conditions to identify closures, seals, or bottle constructions that may fail before the product reaches the consumer.
Standard reference: ASTM D4169 (USA) and ISTA 2A (international e-commerce) are the most commonly applied transit standards. Your logistics provider or target retailer may specify a particular standard.
Thermal cycling: Products shipped by air freight may experience temperatures below -10°C in cargo holds and above 40°C in surface transport. A 3-cycle thermal test (-10°C / +40°C / ambient, 4 hours per phase) reveals closures or materials that crack or leak at temperature extremes.
Vibration and drop: Palletised vibration testing simulates road freight. Individual drop testing simulates handling in fulfilment centres and consumer unboxing.
Airless Bottle Specific Tests
Airless pump bottles require additional testing beyond standard pump and transit testing because of the piston mechanism. The piston must move smoothly throughout the product’s fill life while maintaining adequate contact with the bottle bore to minimise air ingress during dispensing.
Piston movement test: Fill an airless bottle with the actual formula. Dispense a defined number of strokes and measure piston position. Confirm that the piston moves at a consistent rate and does not bind or skip. Repeat at elevated temperature and with the bottle inverted.
Residual product: Document the percentage of formula that cannot be dispensed when the piston has reached its full travel position. Actual residual volume is model-dependent and varies by bottle geometry and formula.
Formula contact components: Confirm the resin of every component that contacts the formula — piston, dip tube, pump actuator, and inner valve components. For formulas with strong solvents, acids, or high-percentage oils, the contact resin compatibility should be confirmed with the packaging manufacturer before ordering samples.
Recommended Testing Timeline Before Mass Production
| Phase | Activity | Duration | When to Do It |
|---|---|---|---|
| Sample receipt | Visual inspection, dimensional check, fill trial | 1–3 days | Immediately on sample receipt |
| Pump dispense test | Prime, output consistency, angle performance | 3–5 days | After fill trial confirms correct fill level |
| Weight loss (fast screen) | 2-week accelerated at 40°C | 2 weeks | Run in parallel with pump test |
| Stress crack screen | 4-week soak at 40°C, inspect weekly | 4 weeks | Start immediately on sample receipt |
| Transit test | ISTA 2A or equivalent | 3–5 days | After weight loss and pump tests pass |
| Full weight loss (12 weeks) | Stability at 40°C / 75% RH | 12 weeks | Run in parallel with production prep |
Minimum recommended testing window before placing a mass production order: 4–6 weeks for a new packaging format. Factor this into your product launch timeline.
Frequently Asked Questions
Does Cosmopacks provide compatibility testing for its packaging?
Cosmopacks can provide sample packages for your in-house or third-party compatibility testing, and can advise on the testing approach appropriate for your formulation type and target market based on our manufacturing experience. For brands that do not have in-house testing facilities, we can recommend external cosmetic testing laboratories. Contact us at info@cosmopacks.com to discuss your testing requirements alongside your packaging inquiry.
What formula types require the most rigorous compatibility testing?
Formulas that require the most thorough compatibility testing include: high-alcohol products (>20% ethanol or IPA) — weight loss and seal integrity; oil-based cleansers, facial oils, and anhydrous formulas — stress cracking and pump compatibility; acid-based serums (AHA/BHA, vitamin C, low-pH formulas) — material compatibility and potential corrosion; high-viscosity creams and balms — pump dispense consistency and priming; sunscreen formulas — UV filter compatibility with plastic resins, particularly PP and PETG; and any product with a high fragrance or terpene load — stress cracking in PETG and certain PP grades.
Is compatibility testing required by FDA or EU cosmetic regulations?
Neither FDA (USA) nor the EU Cosmetics Regulation (EC 1223/2009) mandates a specific compatibility test protocol by name. However, both regulatory frameworks require that cosmetic products be safe for use, which includes packaging safety. EU Cosmetics Regulation requires a Cosmetic Product Safety Report (CPSR) that covers packaging compatibility as part of the safety assessment. In practice, brands selling in regulated markets need documented evidence that their packaging performs safely with their formulation — compatibility testing provides that evidence.
How many samples do I need to run a full compatibility test?
A standard pre-production compatibility test protocol typically requires between 30 and 60 filled samples per test condition. For example: 10 samples upright / 10 inverted for weight loss at 40°C; 10 samples for stress crack evaluation; 10 samples for transit testing; and a reserve set for any repeat or extended testing needed. Request at least 60–100 samples per packaging option when placing a pre-production sample order if you intend to run a full protocol.
Can I run compatibility testing before finalising the decoration on my packaging?
Yes — and this is recommended. Compatibility testing should be run on undecorated or pre-production samples (same resin, same construction, same closure system as the production specification) so that results are available before committing to the decoration and production investment. Surface treatments such as coating, UV lacquer, or metallisation can in some cases affect the results of certain tests, so your testing plan should account for this if a surface treatment is specified.
Why Packaging Compatibility Testing Is Not Optional
The cosmetic industry regularly encounters packaging failures that could have been identified during pre-production testing. The financial consequences of discovering a failure after mass production — failed goods, recall risk, customer returns, and brand damage – are substantially higher than the cost of a structured pre-production qualification process.
The most common categories of packaging failure that compatibility testing is designed to catch:
Weight loss and evaporation – alcohol-based formulas, including toners, setting sprays, and hand sanitisers, can lose significant weight through the shoulder or closure of a bottle over time if the sealing system is not appropriate for alcohol-containing products.
Stress cracking – some plastic resins, particularly PETG and certain grades of PET, can develop micro-cracks or visible crazing when in contact with specific surfactants, essential oils, fragrance components, or solvents. This failure may not appear immediately – it can develop over weeks or months of contact.
Pump incompatibility with formulation viscosity – a pump designed for a medium-viscosity serum may fail to prime or dispense consistently with a thick cream or a very thin, water-like toner. Pump output can vary significantly with formulation viscosity, and this must be tested with the actual formula before mass production.
Leakage during transit – e-commerce and international shipping subject packaging to temperature cycling, pressure changes, and physical shock that retail shelf distribution does not. A closure system that performs correctly at ambient temperature in a warehouse may leak during air freight or when stored in a warm fulfilment centre.
Discolouration and formula interaction – contact between the formula and plastic components (dip tube, pump mechanism, piston) can cause discolouration, cloudiness, or formulation instability in some cases. This is particularly relevant for formulas containing strong acids, retinoids, or vitamin C derivatives.
Need Samples for Compatibility Testing?
Cosmopacks supplies pre-production samples for compatibility evaluation with all new packaging inquiries. Tell us your formulation type and packaging format — we’ll help you identify the right test protocol and sample quantity for your project.